Replacing Part of the Malt: Alpha and Beta Amylase for Adjunct and Barley Mashes
For breweries and malt-extract producers mashing unmalted barley or adjuncts: where beta-amylase fits, the rest and pH window, what to trial, and what to send for a quote.
Brewhouses that swap part of their malt for unmalted barley or other adjuncts lose some of the malt's own enzymes, and the gap shows up as slower conversion and less fermentable wort. This guide is for brewers, malt-extract producers and the distributors who supply them: why plants add amylases when they cut malt, how the beta-amylase rest is run, and how to trial a grade and request a quote before you order by the drum.
Why plants add enzymes when they cut malt
During malting, barley builds up its own hydrolytic enzymes, and in the mash those enzymes, or added ones, break starch and protein down into soluble small molecules. With a normal malt grist, the extract rate can reach about 80 percent. Some plants replace more than half of the malt with raw barley and add enzyme preparations instead; the extract rate on that route is only 67 to 69 percent, but the beer shows good foam and higher non-biological stability.
As enzyme supply has grown, more brewhouses saccharify with added enzymes, because the cycle is shorter, extract recovery rises and stability is easier to control. Added enzymes are used mainly to treat adjuncts and to make up for activities the malt is short of. The enzymes in common use are an alpha-type liquefying enzyme, beta-amylase, beta-glucanase, neutral protease and compound blends.
For a buyer the decision is a trade: cheaper grain against lost extract, so the enzyme program is priced against the extract and stability your own trial delivers.
Running the beta-amylase rest
Mash thickness is usually held at a malt-to-water ratio between 1:2.5 and 1:4.0. Saccharification runs for 40 to 60 minutes so that beta-amylase can do its full work, then the mash is raised to 70 °C for about five minutes while the liquefying and saccharifying enzymes keep acting. A mash pH of 5.2 to 5.8 is the usual compromise, and judged by conversion speed and the final sugar mix, a wort strength of 14 to 18 percent sugar is preferred.
The factors that move conversion are malt quality and grind, saccharification temperature and time, mash pH and mash concentration. Grind the malt so the husk breaks without shattering, which keeps husk material out of the wort, while the endosperm is milled as fine as practical. Keep the beta-amylase rest ahead of the hotter step: an early hot step shortens the time the enzyme has to build maltose.
Alpha or beta: which one is short in an adjunct mash?
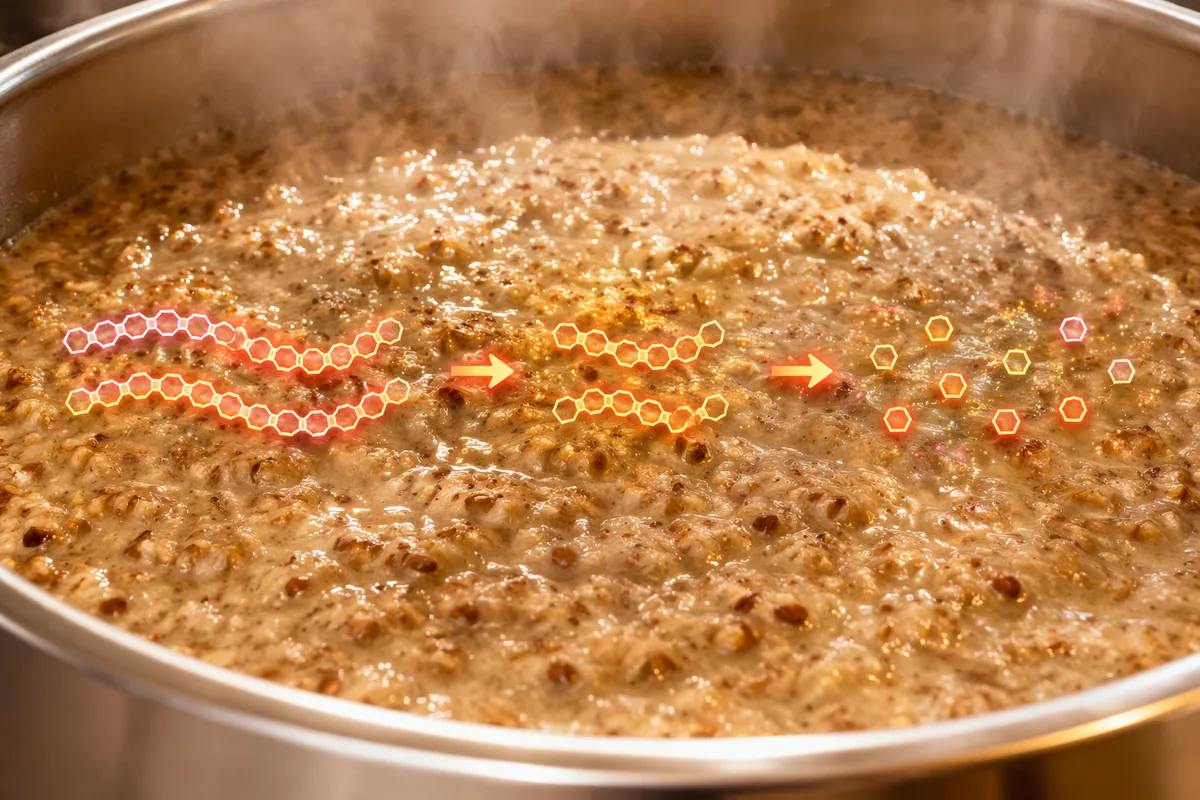
Beta amylase is most valuable when the mash needs additional saccharifying power after starch has been made accessible. In adjunct brewing, raw material pre-treatment and gelatinization are often the limiting steps; beta amylase cannot efficiently convert ungelatinized starch or bypass alpha-1,6 branch points. A thermostable alpha amylase may be used earlier for liquefaction, followed by a beta-amylase rest to increase maltose. In high-gravity brewing, the goal may be higher fermentable extract without excessive viscosity or unpredictable attenuation. The enzyme program should match yeast capability, beer style, and downstream filtration or separation limits. For malt extract and syrup production connected to brewing supply chains, beta amylase can support maltose-rich profiles, but specifications should state target DE, maltose percentage, solids, color, and flavor constraints before enzyme selection.
Use alpha amylase where liquefaction or viscosity control is limiting. • Use beta amylase where maltose formation and fermentability are limiting. • Define sugar-profile targets before locking dosage and mash schedule. • Validate adjunct pre-treatment before blaming enzyme performance.
Troubleshooting low maltose or poor attenuation
If maltose is below target, first determine whether the issue is enzyme activity, substrate access, or process control. Poor milling can reduce extract availability, while excessive heat can inactivate beta amylase before sufficient saccharification occurs. Incorrect mash pH may also suppress activity, especially if water chemistry or adjunct loading changes. When trialling beta amylase from a new supplier, compare it against a retained reference lot under identical bench conditions rather than relying only on plant-scale impressions. Measure maltose, glucose, maltotriose, limit dextrins, real degree of fermentation, viscosity, and iodine conversion. If attenuation is too high, the dosage or rest time may be excessive for the beer style. If attenuation remains low despite higher enzyme dose, the limiting factor may be alpha amylase activity, gelatinization, mash mixing, or yeast performance rather than beta amylase itself.
Check actual pH, temperature profile, and hold time • Run side-by-side trials against current enzyme or malt-only control • Review sugar profile before changing production-scale dosage • Separate mash conversion problems from fermentation problems
Trial plan before you order
Beta-amylase dosage must be set against the supplier's declared activity, process temperature, grist composition, residence time, and target fermentability. Product weight alone is not comparable between suppliers, so ask for the screening band in activity units on the TDS. Start with a control mash, then run at least three dosages under identical mash thickness, pH, calcium level, and rest time. Measure wort gravity, maltose, glucose, maltotriose, limit dextrins, viscosity, iodine reaction, and fermentation attenuation. The best dose is not the highest conversion result; it is the lowest reliable dose that reaches the beer specification without negative flavor, filtration, or cost impact.
Confirm dosage on an activity-unit basis. • Run control, low, medium, and high enzyme treatments. • Calculate cost-in-use per hectoliter or per metric ton of grist. • Avoid overdosing if fermentability and filtration targets are already met.
QC checks, pilot validation, and supplier qualification
Industrial enzyme buying should combine technical fit with supply assurance. Before approval, request the COA for the offered lot, a TDS with activity definition and recommended use range, and an SDS for safe handling and storage. The COA should identify lot number, activity result, appearance, and relevant quality tests stated by the supplier. In pilot validation, compare enzyme lots against a no-enzyme control and the current process benchmark. Track sugar profile by HPLC or equivalent method where available, plus iodine test, extract, viscosity, filtration time, fermentation kinetics, RDF or ADF, and sensory risk notes. Supplier qualification should also review batch-to-batch consistency, lead time, packaging, storage temperature, shelf life, documentation responsiveness, and change notification practices. For alpha amylase beta amylase brewing programs, approve the enzyme only after pilot data supports specification, economics, and brewery operability.
Request COA, TDS, SDS, and lot traceability. • Validate in pilot mash and fermentation, not only bench starch tests. • Compare cost-in-use against extract gain and attenuation improvement. • Document storage and handling requirements before scale-up.
Technical Buying Checklist
Adjunct type and share of the grist (raw barley, rice, corn grits or other), and whether it is cooked before mashing. • Malt quality and grind for the current lot. • Target extract, fermentability and wort strength for the beer or malt extract you sell. • Mash schedule: thickness, beta-amylase rest length, the hotter step and mash pH. • Which enzymes the grist is short of: liquefying, saccharifying, beta-glucanase or protease. • Activity definition and screening band from the TDS, so offers can be compared per unit of activity. • For the quote: product or grade, quantity per order or per month, and destination country.
Beta-Amylase for Research & Industry
Need Beta-Amylase for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
Can added enzymes replace part of the malt?
Yes. Some plants replace more than half of the malt with raw barley and add enzyme preparations. The extract rate on that route is 67 to 69 percent against about 80 percent for a malt grist, but the beer shows good foam and higher non-biological stability. Price the enzyme program against the extract your own trial delivers.
Can beta-amylase do the liquefying job of alpha-amylase?
Usually not. Beta amylase needs accessible gelatinized starch or suitable dextrins and does not perform the same liquefaction role as alpha amylase. With high-adjunct mashes, alpha amylase may be required to reduce viscosity and create shorter substrates before beta amylase builds maltose. Pilot trials should compare alpha-only, beta-only, combined enzyme, and no-enzyme controls under the actual brewhouse conditions.
How long should the beta-amylase rest run?
A common schedule saccharifies for 40 to 60 minutes so beta-amylase can do its full work, then raises the mash to 70 °C for about five minutes, with mash pH between 5.2 and 5.8. Confirm the schedule on your own grist in a pilot mash.
Which sugar does beta-amylase mainly release?
Beta-amylase mainly releases maltose, not glucose. Glucose levels in wort are influenced by raw material, mash conditions, malt enzymes, and any glucoamylase or related activities present. For troubleshooting, use HPLC or an equivalent sugar method to distinguish glucose, maltose, maltotriose, and residual dextrins.
What should we send for a quote?
The product or grade, the quantity per order or per month, and the destination country, plus the adjunct type and share, your mash schedule and the beer or malt-extract specification you need to hit. Distributors can list the end markets they serve. Price and lead time are quoted per order.
Related: Beta Amylase for Brewing Mash — Maltose Generation for Beer and Ale
Request beta-amylase specifications, pilot dosage guidance, and a cost-in-use review for your brewing process. The application page on beta amylase for brewing mash lists specs, MOQ, and a free 50 g sample.
Contact Us to Contributehello@mail.betaamylase.bio